
As a maintenance or production manager, you regularly decide how much maintenance effort each piece of equipment actually needs, and where paper or Excel reach their limits. Without a clear framework, this quickly leads to poorly calibrated intervals, gaps in documentation, and KPIs you cannot fully trust. This article maps out the relevant strategies, metrics, and selection criteria so you can evaluate and improve your own maintenance practice with confidence.
Key takeaways
Risk-based planning by criticality beats fixed maintenance intervals applied equally across all equipment.
Periodic, condition-based, and predictive maintenance each suit different equipment types and data situations.
MTTR, MTBF, and OEE show whether a chosen strategy actually works.
Digital maintenance plans and documentation close the typical gaps that paper and Excel leave in traceability and audits.
A step-by-step pilot approach with clear criteria makes it easier to choose the right software solution.
What Is Preventive Maintenance?
Preventive maintenance covers planned measures a company carries out before an equipment fault or failure occurs. Digital preventive maintenance manages these measures through equipment-specific maintenance plans, clear responsibilities, and complete error documentation.
The goal is to avoid unplanned downtime, increase equipment availability, and limit the costs of repairs, spare parts, and lost production. To achieve this, maintenance and production teams carry out inspections, servicing, and the proactive replacement of worn components.
Prevention does not mean maintaining every machine as often as possible. An economical strategy sets the frequency and scope of maintenance according to failure risk. What matters most is the criticality of the equipment, the likelihood of a defect, and the possible consequences for safety, quality, delivery dates, and production costs.
Digital systems support this risk-based planning. They connect equipment master data, maintenance intervals, work instructions, measured values, spare parts, and execution records. This creates a closed loop from planning through execution to evaluation.
How Does Preventive Maintenance Work?
Preventive maintenance follows a recurring cycle: assess risks, plan measures, carry out the work on schedule, document the results, and refine the intervals based on the data gathered. The trigger is a defined point in time, a usage limit, or an observed equipment condition.
Typical triggers include calendar days, operating hours, load cycles, units produced, or condition thresholds. A maintenance plan defines which task needs to be carried out on which piece of equipment, who is responsible, and which tools, spare parts, or safety measures are required.
Typical measures include:
Inspections: Skilled technicians or qualified production staff assess the current condition and record any deviations.
Servicing: Cleaning, lubrication, adjustment, and the replacement of defined wear parts slow down wear.
Preventive repairs: Maintenance fixes identified damage before the equipment loses its function.
Preventive replacement: The team replaces components based on runtime, load cycle count, or condition findings.
Improvement measures: Technical or organizational changes increase reliability, maintainability, or safety without changing the equipment's required core function. Examples include more accessible lubrication points, poka-yoke solutions, and more robust bearings.
In practice, a criticality analysis is a good starting point. An FMEA, a risk matrix, or an evaluation of past failures shows which equipment needs a solid maintenance plan first. A highly critical filling line calls for a different strategy than a redundant, inexpensive auxiliary unit.
What Basic Maintenance Activities Does DIN 31051 Define?
According to DIN 31051, maintenance is divided into four basic activities: inspection, servicing, repair, and improvement.
The four activities serve different purposes:
Inspection: Maintenance determines and assesses the current condition. This includes visual checks, functional tests, and measurements of temperature, pressure, vibration, or wear.
Servicing: The team slows the decline of the current condition. Typical tasks include cleaning, lubricating, adjusting, and the scheduled replacement of consumables.
Repair: Maintenance restores the required function after an identified fault or damage. In a preventive process, this happens before a complete functional failure whenever possible.
Improvement: Technical or organizational changes increase reliability, maintainability, or safety without changing the equipment's required core function. Examples include more accessible lubrication points, poka-yoke solutions, and more robust bearings.
These terms should stay clearly separated in maintenance plans. The most common mistake is labeling every activity as servicing. That makes it harder later to analyze effort, root causes of failure, and potential improvements.
How Do Preventive, Corrective, and Predictive Maintenance Differ?
Corrective maintenance responds to a fault that has already occurred, preventive maintenance acts before a failure happens, and predictive maintenance forecasts the expected time of failure. The three approaches differ mainly in their trigger and the amount of data they require.
| Approach | Guiding principle | Trigger | Suited for | Key limitation |
|---|---|---|---|---|
| Corrective maintenance | Repair once something breaks | Loss of function or a fault | Non-critical, redundant, and cheaply replaceable equipment | Unplanned downtime and follow-on damage |
| Preventive maintenance | Act before something breaks | Schedule, usage, or a defined condition threshold | Equipment with known wear patterns and relevant failure consequences | Risk of intervening too early or unnecessarily |
| Predictive maintenance | Know when something will break | Forecast based on condition and process data | Critical equipment with measurable failure indicators and a sufficient data base | Higher effort for sensors, data quality, and models |
Condition-based and predictive maintenance are not the same thing. Condition-based maintenance reacts to a current measured value or threshold. Predictive maintenance uses data series and models to forecast how the condition will develop or how much useful life remains.
No single strategy is economical for every piece of equipment. For a simple, redundant pump, a corrective approach may work well, as long as its failure does not threaten safety or delivery capability. For a gearbox with known wear patterns, a preventive plan usually makes more sense. For a critical spindle with available vibration and temperature data, it is worth examining a predictive approach.
Recommendation: Segment your machine fleet by criticality, failure consequences, and measurability. A risk-based mix of strategies is more economical than applying one single approach across the board.
What Role Does Preventive Maintenance Play as the Third Pillar of Total Productive Maintenance?
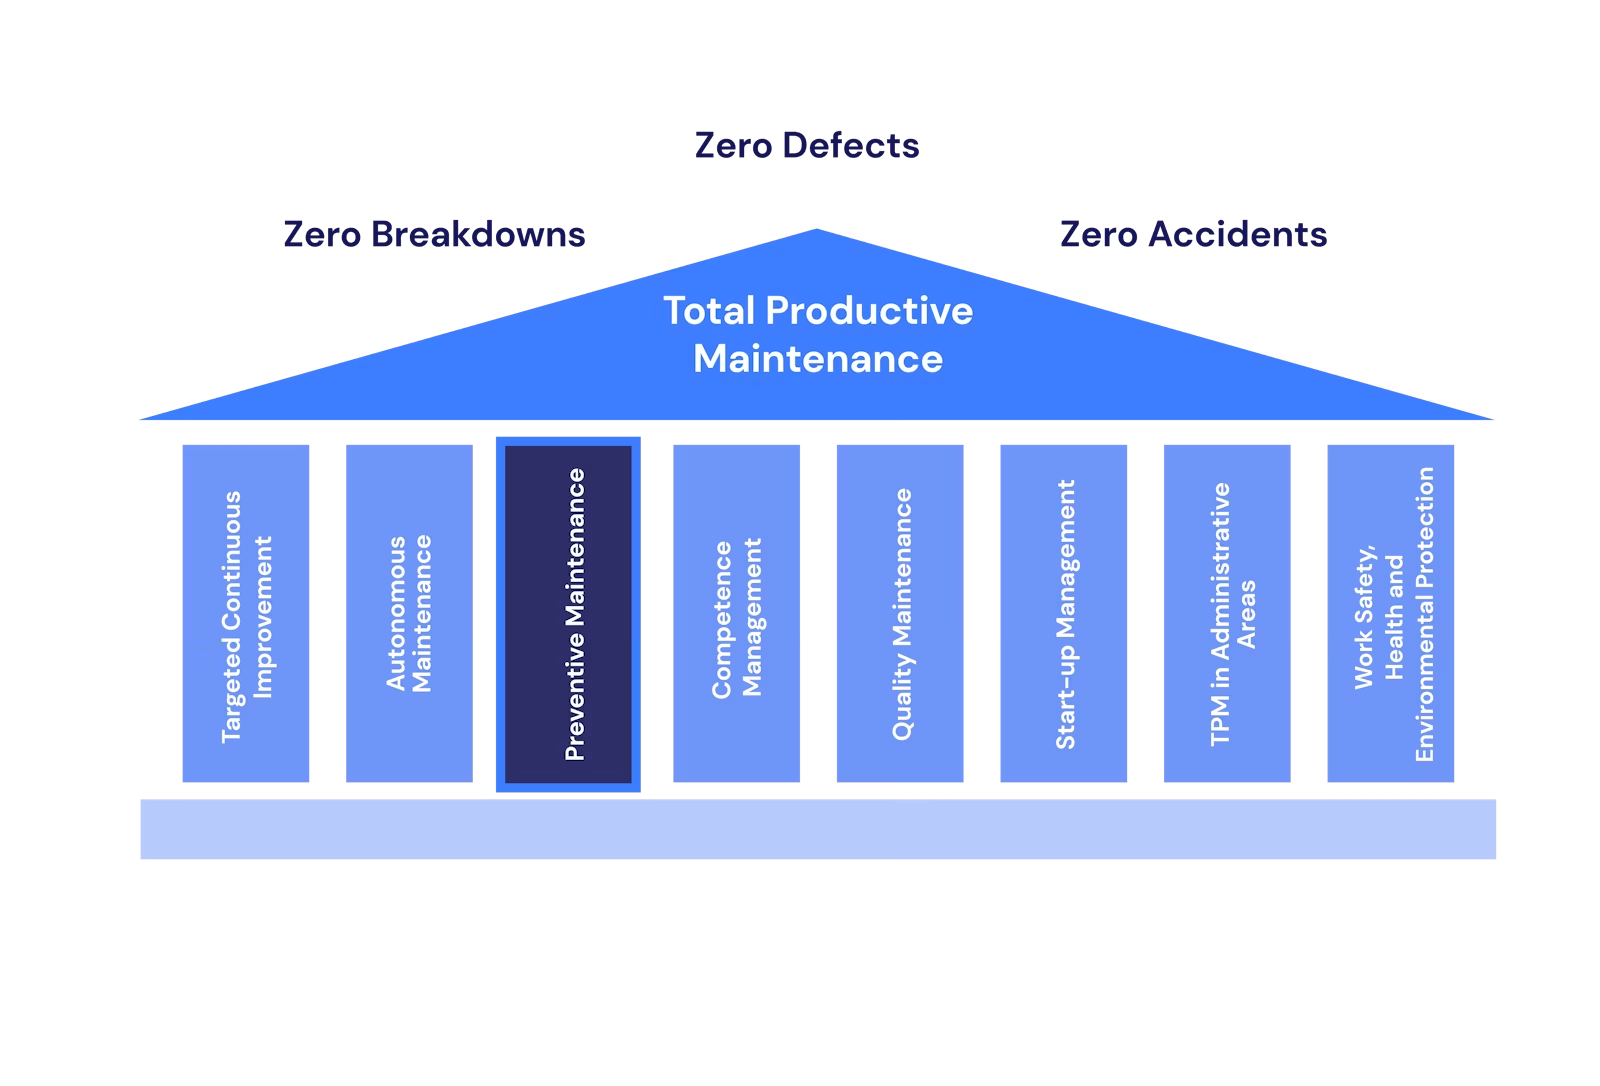
In the commonly used eight-pillar model of Total Productive Maintenance, planned and preventive maintenance forms the third pillar. It creates stable equipment conditions and supports TPM's zero-defects, zero-breakdowns, and zero-accidents goals.
TPM does not treat equipment reliability as the sole responsibility of the maintenance department. Production, maintenance, quality assurance, and management all share that responsibility. Production staff spot and report deviations early, while specialist maintenance teams handle complex inspections, repairs, analyses, and technical improvements.
Preventive maintenance forms the plannable backbone of this approach. It turns manufacturer specifications, experience, and failure analyses into binding work plans. Autonomous maintenance complements this with simple shopfloor tasks such as cleaning, checking, and lubricating.
TPM's zero goals are guiding principles, not a guarantee of fully fault-free operation. Their value lies in a consistent focus on preventing errors, stabilizing processes, achieving 100 percent quality, and maintaining safe working conditions. A closer look at the TPM concept places preventive maintenance within the other pillars and the continuous improvement process.
How Do Periodic and Condition-Based Maintenance Differ?
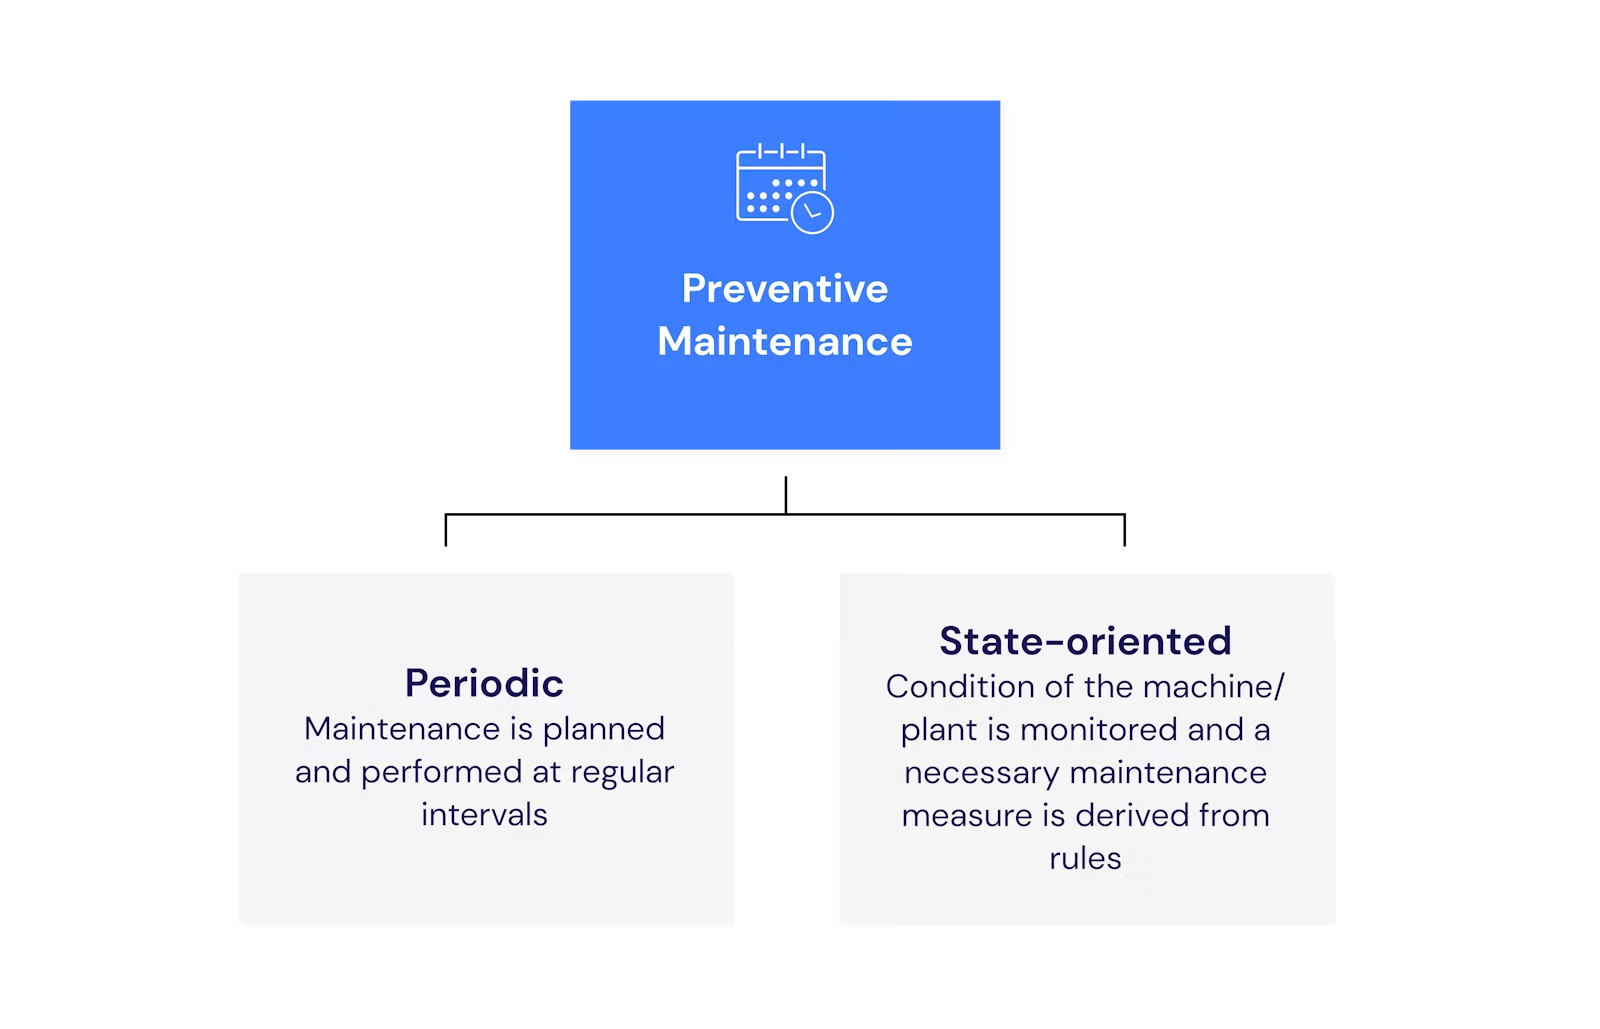
Periodic maintenance triggers tasks at fixed time or usage intervals. Condition-based maintenance triggers an intervention when inspections or measured values indicate a defined need for action.
| Criterion | Periodic maintenance | Condition-based maintenance |
|---|---|---|
| Trigger | Calendar time, operating hours, load cycles, or unit count | Measured value, visual finding, or condition threshold |
| Data basis | Manufacturer specifications, experience, and maintenance history | Current condition data and defined thresholds |
| Typical examples | Oil changes, filter changes, safety inspections | Bearing diagnostics, tool wear, filter condition |
| Strength | Easy to plan and standardize | Interventions match actual wear |
| Risk | Maintenance performed too early or too late | Missed faults with unsuitable metrics or poor data quality |
| Requirement | Reliable intervals and available maintenance windows | Measurable failure indicator, suitable inspection technology, and clear response rules |
In many manufacturing operations, a hybrid approach works best. Safety-relevant checks and mandatory servicing stay tied to fixed intervals. The team monitors wear-dependent components based on their actual condition as well.
Recommendation: Use periodic plans for stable and well-understood wear patterns. Switch to condition-based maintenance when load and wear fluctuate significantly and a reliable condition indicator is available.
When Does Periodic Maintenance on Fixed Intervals Make Sense?
Periodic maintenance suits equipment with predictable wear, clear manufacturer guidelines, and manageable maintenance costs. A maintenance calendar triggers the work at set points in time or after defined usage values are reached.
Intervals come from operating manuals, legal or internal inspection requirements, and a company's own experience data. Besides calendar days, operating hours, shifts, load cycles, or units produced also serve as triggers.
This approach fits especially well with standardized tasks such as lubrication, filter changes, calibration, or the replacement of cheaply available wear parts. It also suits machines that rarely fail and whose repair does not trigger critical production consequences.
Regularly reviewing the intervals is essential. A manufacturer's plan applied unchanged ignores actual utilization, as well as dust, temperature, shift patterns, and product variants. Intervals that are too short create unnecessary cost and intervention risk. Intervals that are too long raise the probability of failure.
When Does Condition-Based Maintenance by Machine State Make Sense?
Condition-based maintenance suits equipment with fluctuating load, many wear parts, and measurable early warning signs of failure. The team steps in as soon as inspections or measured values indicate a relevant decline in condition.
Typical metrics include:
Temperature of bearings, motors, or lubricants
Vibration and noise from rotating components
Pressure and flow in hydraulic or pneumatic systems
Fill levels and particle contamination of operating fluids
Speed, current draw, and torque
Tool wear, play, leakage, or surface condition
Thresholds need a technical justification. A single alarm value is often not enough for dynamic processes. Trend data, machine load, product variant, and ambient conditions all provide context for a reliable assessment.
Not every condition monitoring setup requires additional sensors. Standardized visual checks, leak inspections, and measurements with handheld devices deliver enough usable data for many pieces of equipment. Permanent sensors pay off mainly for critical, hard-to-access, or continuously running equipment.
What Benefits Does Preventive Maintenance Bring for Productivity?
Preventive maintenance increases productivity when it reduces unplanned downtime and follow-on damage by more than the planned maintenance time and resources it consumes. It also improves the predictability of staffing, spare parts, and production windows.
The key benefits are:
Higher equipment availability: The team spots wear and deviations before they cause an extended stoppage.
Less follow-on damage: A bearing replaced in time protects the shaft, housing, and adjacent components.
Predictable costs: Purchasing and maintenance can plan spare parts, tools, and staff ahead of the intervention.
Shorter working times: Recurring, standardized tasks cut search time and improvisation.
More stable process quality: Well-maintained tools, guides, sensors, and dosing systems keep process parameters within specification.
Longer service life: Proper lubrication, cleaning, and adjustment slow down component wear.
Better workplace safety: Planned interventions with lockout procedures, risk assessments, and appropriate qualifications replace rushed emergency repairs.
Higher resilience: Fewer unplanned failures stabilize delivery dates and reduce dependence on spare parts that must be sourced at short notice.
Prevention does not automatically cut total maintenance costs, though. Interventions that are too frequent, poorly chosen intervals, and unnecessary part replacements all drive up cost. In practice, the risk-based optimization of maintenance plans is what determines economic success.
How Does Preventive Maintenance Affect Overall Equipment Effectiveness (OEE)?
Preventive maintenance improves OEE mainly through higher availability. Stable equipment conditions also affect performance and the quality rate, because micro-stoppages, speed losses, and process-related scrap all decrease.
OEE looks at three factors: availability, performance, and quality. An extended unplanned failure directly hits availability. Dirty sensors, worn guides, or under-lubricated components also cause reduced speeds, short stops, and quality deviations.
Planned maintenance work carried out within scheduled production time still counts as downtime at first. Its economic value comes from preventing longer unplanned failures or recurring performance losses. Companies should therefore align maintenance windows with production planning and shift leadership, rather than dress up OEE by simply shifting time boundaries on paper.
For effective control, it helps to look at OEE losses, root causes of failure, and maintenance data together. Pareto analyses show which equipment and failure patterns cause the biggest productivity loss. An Ishikawa analysis or 8D process then helps with recurring and complex faults.
How Do You Measure Success With MTTR and MTBF?
MTTR measures the average repair time, while MTBF measures the average operating time between two failures. An effective maintenance strategy aims for a shorter MTTR and a higher MTBF.
These metrics serve different purposes:
MTTR, Mean Time to Repair: This metric describes how long the team typically needs to restore functionality after a failure. Standardized diagnostic procedures, available spare parts, clear work instructions, and qualified staff all lower MTTR.
MTBF, Mean Time Between Failures: For repairable equipment, this metric describes the average operating time between two failures. Improved maintenance plans, eliminated weak points, and robust operating conditions all raise MTBF.
Reliable comparisons require clear measurement rules. Whoever is responsible must define when a failure begins, when the equipment counts as ready for production again, and which wait times count toward MTTR. MTBF likewise needs consistently defined failure types and operating times.
MTTR and MTBF should not be assessed in isolation. A high MTBF is a positive sign, but it says nothing about maintenance costs or planned downtime. Useful additions include the share of maintenance orders completed on time, the number of overdue tasks, the share of emergency orders, recurring faults, and maintenance cost per piece of equipment or operating hour.
In practice, it helps to break results down by equipment class and failure pattern. A plant-wide average hides the differences between a critical machining center, material handling equipment, and simple auxiliary units.
What Drawbacks and Risks Does Preventive Maintenance Have?
Preventive maintenance causes planned downtime, staff effort, and material costs. Poorly chosen intervals also lead to unnecessary interventions without fully eliminating the residual risk of unplanned faults.
The key risks are:
Over-maintenance: The team replaces functional parts too early or carries out work more often than technically necessary.
Intervention-related faults: Incorrect assembly, contamination, or faulty adjustment create new problems.
Unsuitable intervals: Rigid calendar plans ignore fluctuating loads and actual wear patterns.
High resource demand: Maintenance planning, execution, documentation, and analysis tie up qualified staff.
Residual risk of spontaneous failures: Electronic defects, operator error, and random damage cannot be prevented through maintenance intervals alone.
False sense of security: Ticked-off checklists are no substitute for proper condition assessment and root cause analysis.
Production conflicts: Missing maintenance windows lead to postponements, overdue tasks, or short-notice interventions during active production runs.
The most common mistake is aiming for maximum rather than optimal maintenance frequency. An FMEA or criticality matrix provides the prioritization needed. Maintenance history, MTBF, findings, and parts consumption then show whether an interval should be extended, shortened, or replaced with condition monitoring.
Why Does Preventive Maintenance Often Fail With Paper and Excel?
Paper and isolated Excel files make it hard to centrally manage, version, and evaluate preventive maintenance. As the number of assets grows, this creates media breaks, documentation gaps, and a high manual maintenance workload.
Staff often transfer maintenance instructions from manuals into Word or Excel templates. Every machine variant ends up with its own separate files and checklists. When thresholds, components, or safety requirements change, those responsible then have to update multiple documents.
On the shopfloor, it is often unclear which version is currently valid. Handwritten entries stay incomplete or hard to read. Photos, measured values, and identified deviations sit separately from the actual maintenance record. When this information is later transferred into an ERP or CMMS system, it gets lost or reaches the right person too late.
Excel works for a clearly defined pilot area or a small, stable machine fleet. Its limits show up with multiple plants, many variants, role-specific approvals, automatic due dates, and complex escalation paths. At that point, there is no reliable connection between planning, execution, deviation management, and KPI evaluation.
The point is not to eliminate paper for its own sake. The digital process needs to provide current instructions, validate inputs, and turn a critical finding directly into a follow-up action with a clear owner.
What Are the Consequences of Poor Traceability for Audits and Certifications?
Poor traceability makes it impossible to reliably prove that required maintenance work was completed in full, on time, and according to the valid instruction. This raises the risk of findings in customer, process, and certification audits.
Auditors and customers expect clear answers to key questions: Who carried out which task, when, and on which piece of equipment? Which document version applied? What measured values and deviations were recorded? Who reviewed the result, and what follow-up actions did the company take?
This kind of evidence matters in quality, occupational safety, and customer audits. For production-critical equipment in particular, customers often expect traceable documentation of the maintenance and inspection work performed.
Missing data also undermines internal decisions. Management cannot identify recurring weak points, overdue maintenance, or actual resource needs. As a result, budget, spare parts, and investment decisions end up based on assumptions rather than a consistent maintenance history.
What Do Companies Need Before Introducing Preventive Maintenance?
A solid rollout needs clear responsibilities, well-maintained equipment master data, qualified staff, and binding maintenance windows. Only once these foundations are in place does digitalization create a controllable process, rather than a digital copy of existing chaos.
Before starting, production management, maintenance management, and shift leadership should clarify:
Equipment structure: Which assets, assemblies, and components fall within scope?
Criticality: What impact do failures have on safety, quality, performance, the environment, and delivery capability?
Responsibility: Who creates, reviews, approves, and updates maintenance and inspection plans?
Qualification: Which tasks require a licensed electrician, a mechanic, or other specifically qualified personnel?
Resources: What staffing capacity, spare parts, tools, and inspection equipment are available?
Time windows: When can work be combined with the production schedule, setup processes, and shift changes?
Safety: Which lockout procedures, risk assessments, and personal protective equipment are required?
Data: What failure, runtime, and condition data already exists, and how reliable is it?
Control: Which metrics show schedule adherence, effectiveness, and cost-efficiency?
In practice, a cross-functional ownership model works well. Maintenance owns technical standards and complex interventions. Production plans access and time windows. Quality assurance assesses quality-relevant impacts. IT and information security secure integrations, access rights, and data availability.
What Role Does Autonomous Maintenance by Production Staff Play?
As part of autonomous maintenance, qualified production staff take on simple, clearly defined care and inspection tasks. They spot deviations early, while specialist maintenance teams focus on diagnosis, repair, and technical improvement.
Suitable tasks include cleaning, visual inspection, lubrication, checking fill levels, and verifying clearly defined normal conditions. Visual standards, 5S, illustrated work instructions, and clear reference patterns make safe execution easier.
Autonomous maintenance does not replace specialist technicians. Work on electrical systems, safety equipment, or complex assemblies stays with specialist maintenance, in line with qualification requirements and internal approvals. Every deviation also needs a clear escalation path.
The greatest benefit comes from operators' daily closeness to the equipment. They notice unusual noises, vibrations, leaks, or changes in process behavior earlier than a maintenance team that visits only periodically. A closer look at autonomous maintenance covers roles, qualification levels, and how it fits into TPM.
How Does Digital Preventive Maintenance Succeed in Practice?
Digital preventive maintenance succeeds through a step-by-step, risk-based build-up. Companies should digitize critical equipment and solid processes first, before rolling the approach out across the entire machine fleet.
A practical approach includes these steps:
Prioritize critical equipment: Assess the consequences of failure for safety, quality, delivery reliability, and cost. Start with a clearly defined pilot area.
Clean up equipment master data: Establish a clear hierarchy of plant, line, equipment, and assembly. Standardize naming, identification, and areas of responsibility.
Review maintenance plans: Do not carry over every historical task unchecked. Remove duplicates and justify intervals with manufacturer specifications, experience data, or risk assessments.
Define triggers and response rules: Set calendar intervals, operating hours, load cycles, or condition thresholds. Determine what happens immediately when a critical finding occurs.
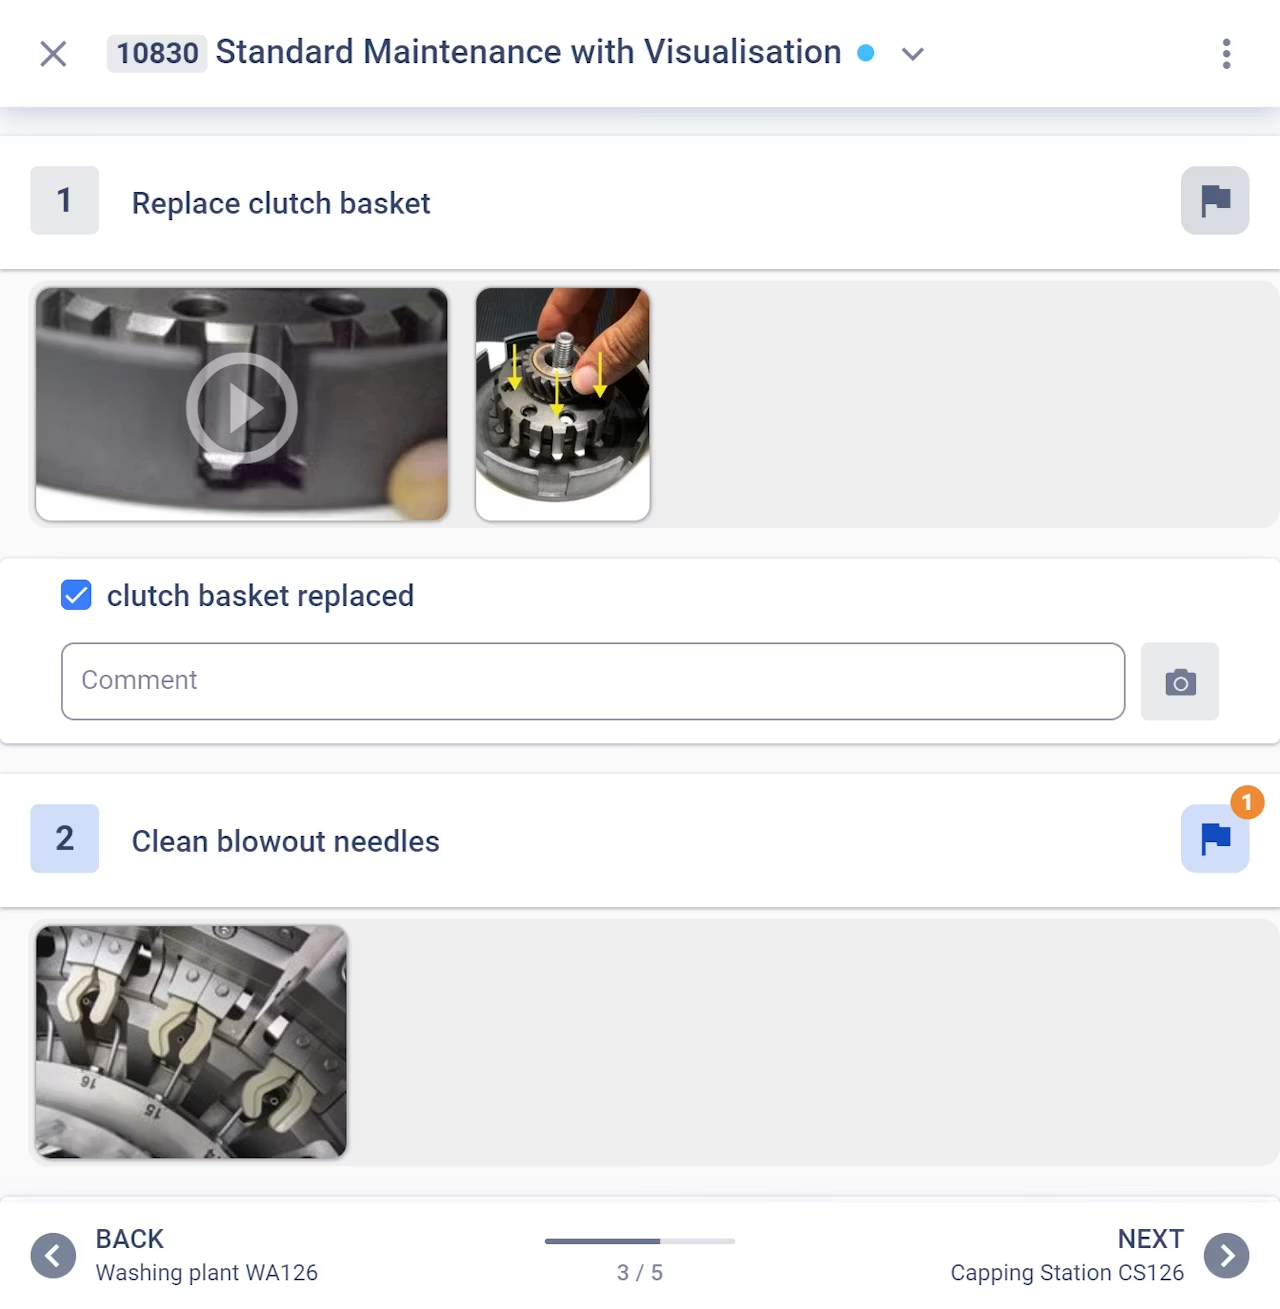
Create digital work instructions: Structure tasks into clear, traceable steps. Add target values, thresholds, safety information, and suitable images or video.
Integrate systems: Connect ERP, MES, and CMMS according to their respective roles. Avoid competing master data and duplicate manual entries.
Pilot and train: Test the process with maintenance staff, machine operators, and shift leadership under real conditions. Train people not just on how to use the system, but on the underlying decision rules.
Evaluate effectiveness and scale: Check schedule adherence, MTTR, MTBF, OEE losses, emergency orders, and recurring faults. Optimize the process before rolling it out to more equipment.
The pilot should cover neither an insignificant secondary asset nor the most complex machine in the plant. A good choice is a relevant piece of equipment with known issues, a manageable scope, and engaged stakeholders. This makes the benefit measurable without burdening the project with unnecessary complexity.
Recommendation: Do not digitize every existing checklist first. Optimize one complete maintenance process, from the due date to the follow-up action, and then apply the proven pattern to further equipment.
How Can Maintenance Plans and Checklists Be Created and Maintained Digitally?
Digital maintenance plans should combine equipment-specific tasks, triggers, thresholds, responsibilities, and escalation paths in a versioned structure. Only reuse existing data from ERP, MES, or CMMS once system ownership and data quality are clearly defined.
A CMMS or EAM system typically manages equipment structure, maintenance planning, orders, spare parts, and cost. ERP handles areas such as materials management and procurement. MES supplies production, runtime, and machine data. A maintenance planning software solution can support the digital planning and execution of maintenance orders, checklists, and records.
A solid digital checklist includes at least:
Clear equipment and component identification
The task's due date and trigger
Required qualification and the responsible role
Safety and lockout information
Work steps in a logical, technically sound order
Target values, tolerances, and clear pass/fail criteria
Mandatory fields for measured values and findings
Photos or videos for steps that need extra explanation
Decision paths for deviations
Proof of execution, review, and approval
With a wide variety of equipment, variant rules work better than many separate copies. The system then presents only the relevant steps based on equipment type, configuration, or assembly. Responsible staff update content centrally and roll it out in a controlled way across the affected maintenance plans.
The key design principle is: as detailed as needed for safe, reproducible execution, but no longer than technically necessary. Overloaded checklists encourage superficial tick-boxing instead of careful condition assessment.
How Do Digital Documentation and Maintenance Reports Improve Audit Readiness?
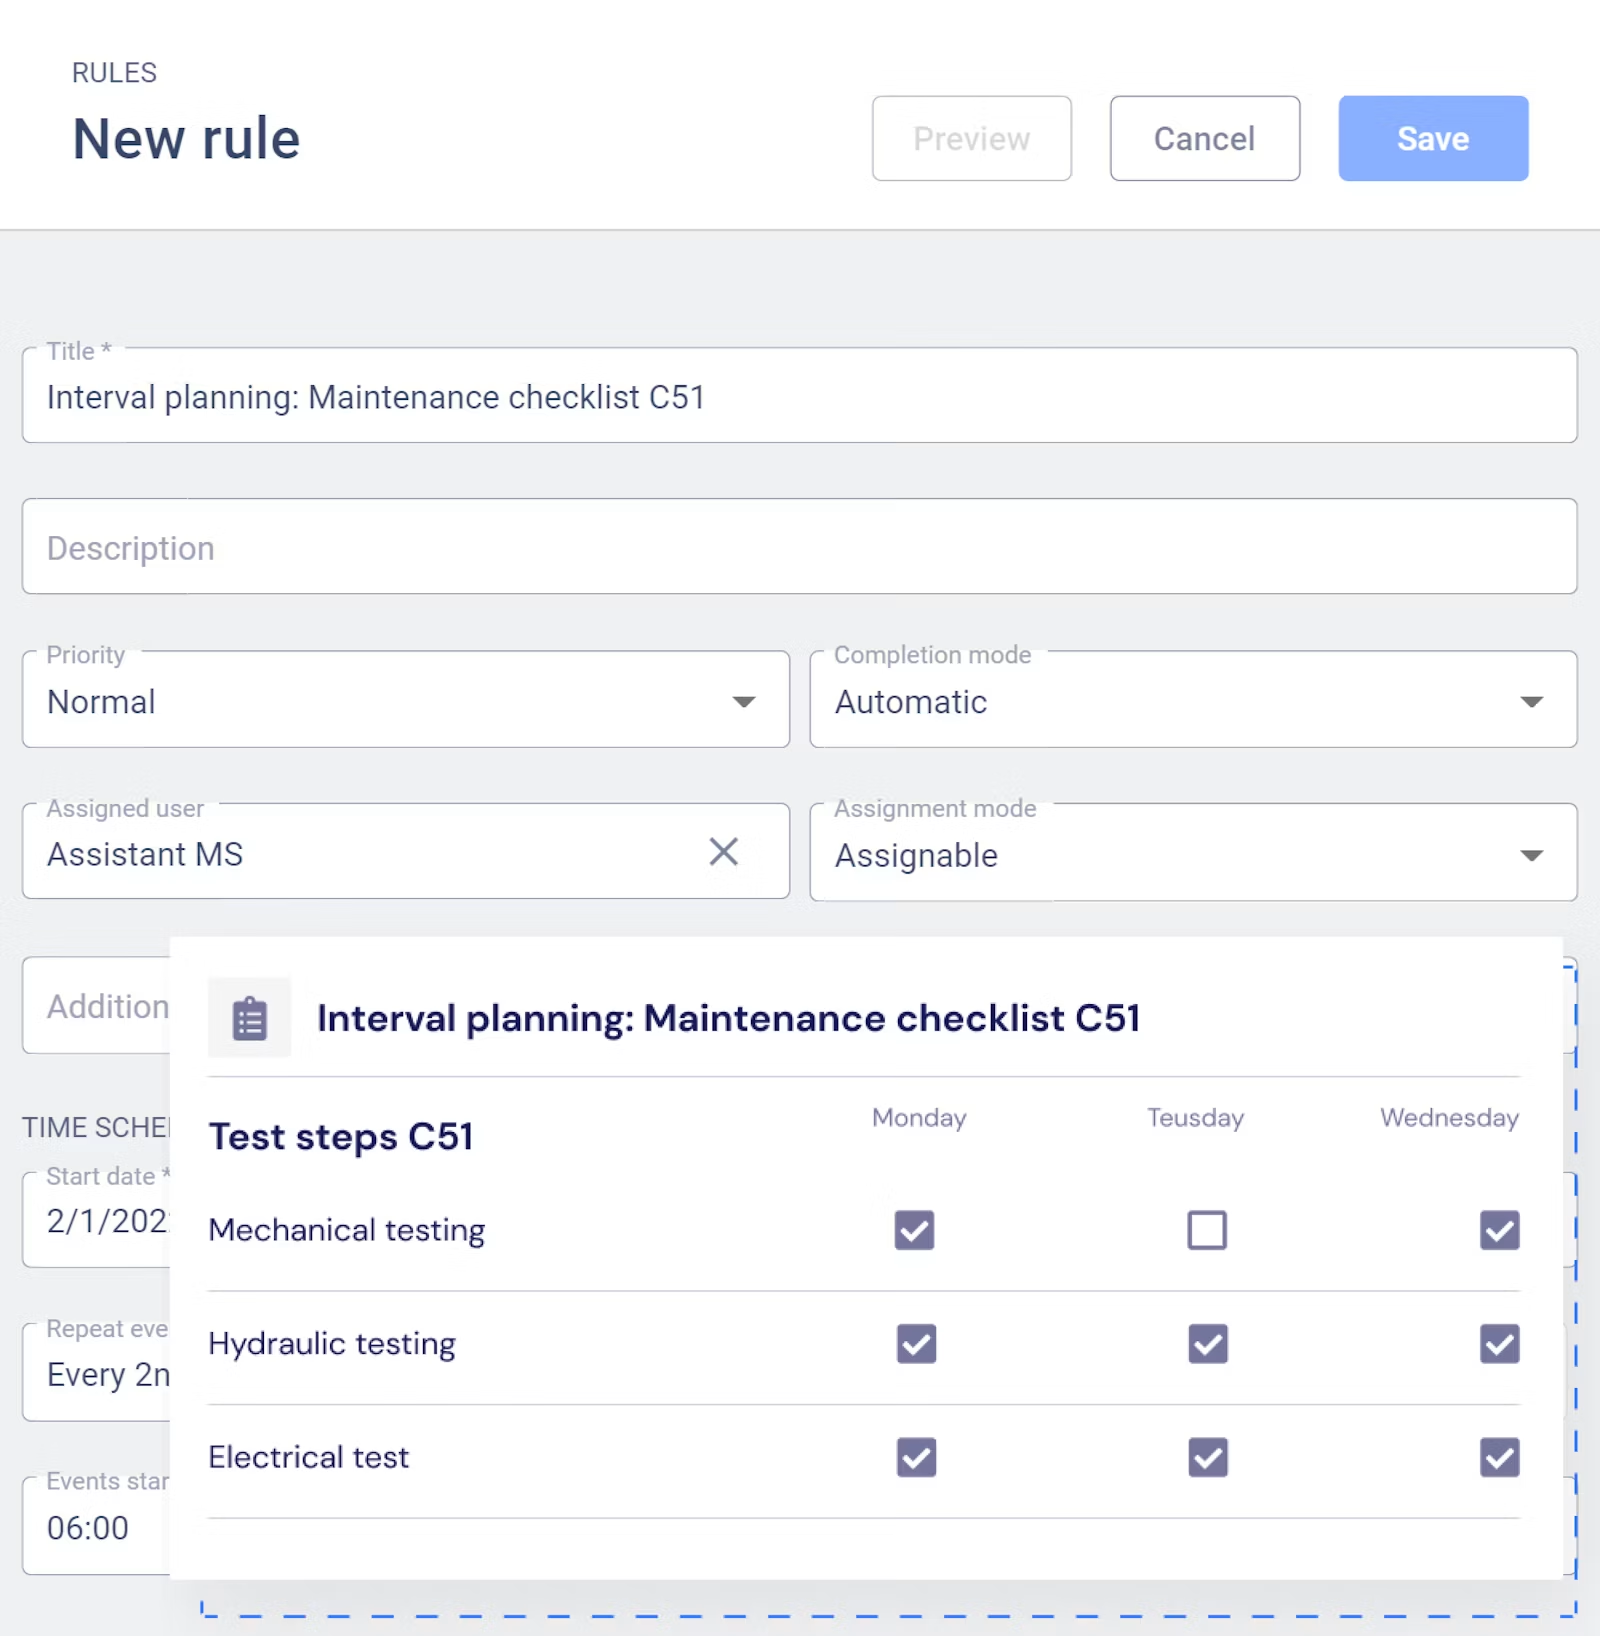
Digital documentation improves traceability when it automatically links execution, measured values, deviations, and approvals to a specific piece of equipment and document version. Automatically generated maintenance reports reduce manual transfer effort and make records available faster.
A solid chain of evidence documents:
The person and role who carried out the work
Equipment, assembly, and location
Date, time, and duration of the task
The version of the work instruction used
Measured values, test results, and photo evidence
Identified deviations
Repair or improvement orders triggered
Review, approval, and closure of the follow-up action
Digital overviews give shift leadership, maintenance management, and senior management visibility into due, overdue, and completed tasks. They also reveal recurring deviations and support preparation for customer and certification audits.
Digital storage alone does not create audit readiness. Companies need role and permission concepts, defined retention periods, traceable versioning, data backup, and controlled change management. The technical completeness of the records matters just as much as the platform itself.
What Criteria Should Guide the Choice of a Digital Solution?
A suitable solution needs to cover the full maintenance process and work reliably on the shopfloor. Integration capability, variant logic, usability, and analyzable data matter more than the longest possible feature list.
The following criteria should factor into the decision:
Integration: Does the solution support data exchange with ERP, MES, CMMS, or EAM systems through documented interfaces?
System ownership: Is it clear which system leads on equipment master data, orders, materials, and execution records?
Variant capability: Can different equipment types, configurations, and assemblies be modeled without uncontrolled document copies?
Usability: Can staff find tasks, target values, and safety information without long searches?
Mobile and stationary use: Does the application work on the intended devices, including in areas with unstable network coverage where needed?
Workflow and escalation: Does a critical finding trigger a notification, an order, or an approval task?
Document control: Are versions, validity, approvals, and change history traceable?
Analysis: Can MTTR, MTBF, schedule adherence, findings, recurring faults, and maintenance effort be analyzed by equipment?
Roles and security: Does the solution support differentiated permissions, authentication, logging, and internal security requirements?
Data access: Can data be exported in a structured format and reused for analysis or a future system change?
Scalability: Do administration and performance stay manageable across multiple plants, languages, and large equipment inventories?
Total cost: Does the assessment cover not just license costs, but also rollout, integration, devices, training, administration, and ongoing upkeep?
Test solutions against real-world scenarios rather than generic demos. Good tests include a due maintenance task, an offline execution, a critical measured value, escalation to maintenance, a schedule change, and retrieving an audit record.
Recommendation: Choose the solution that supports the full closed loop of planning, execution, deviation handling, and evaluation with as few media breaks as possible. A technically extensive platform that lacks shopfloor adoption will not improve maintenance outcomes.
The selection criteria above can be checked directly against Operations1's capabilities.
With the Creator, responsible staff create and version work instructions and maintenance checklists.
Interactions such as numeric inputs with thresholds, photo capture, and signatures record target values and pass/fail criteria directly within the maintenance step.
Rules with configurable intervals generate recurring maintenance orders, so due work does not get lost.
From a critical deviation in a report, the Task module can create an assigned follow-up task with clear status tracking.
The multilevel review process makes the approval of new document versions traceable.
Reports link recorded values to the order and document version and provide filterable records along with a change history.
Order connectors pull maintenance and repair orders from existing ERP or MES systems, while the permission system governs role-based access rights.
If you want to explore how a specific maintenance process could work as a pilot, you can discuss that use case with the Operations1 team.
How Does Digital Preventive Maintenance Secure Productivity and Future Readiness?
Digital preventive maintenance connects planned maintenance with current condition data, standardized execution, and traceable results. Implemented well, it increases equipment availability, stabilizes productivity, and strengthens the resilience of manufacturing operations.
The economic benefit does not come from digital checklists alone. What matters is a risk-based maintenance strategy, clear responsibilities, qualified staff, and a closed flow of information between the shopfloor, maintenance, and management.
Periodic maintenance remains a good fit for stable wear patterns and binding intervals. Condition-based maintenance has the edge when load fluctuates and measurable failure indicators are available. Predictive models complement these approaches wherever criticality and data quality justify the extra effort.
Companies should therefore start with critical equipment, clean up maintenance plans on technical merit, and measure effectiveness through OEE losses, MTTR, MTBF, and recurring faults. That is how digital preventive maintenance becomes an ongoing, continuously improved management process, rather than a one-off digitalization project.