
If you are prioritizing digitalization projects on the shopfloor or planning to introduce a worker assistance system, you need to know which lean principles actually apply and where unnecessary steps can disappear. Without a clear link between the five lean principles and the functions of digital worker guidance, you risk investing in isolated solutions that ease individual symptoms without stabilizing the value stream. This article maps value, value stream, flow, pull and perfection systematically to digital worker guidance and shows where your investment delivers the greatest leverage.
Key takeaways
The five principles, value, value stream, flow, pull and perfection, build on each other and only work together.
Paper-based instructions interrupt flow especially often and make reliable feedback harder to achieve.
Digital worker guidance makes waiting times, error sources and improvement potential visible across the value stream.
Pull control needs stable processes, not just a system switch.
Selecting a worker assistance system should start with process requirements, not a long feature list.
What is lean production?
Lean production is a lean manufacturing approach that minimizes waste, aligns value creation consistently with the customer and improves productivity. The lean production principles help manufacturing companies shorten lead times, stabilize processes and respond faster to changing demand.
Lean production, also called lean manufacturing, looks at the entire path from customer order to finished product. The focus is not on maximizing the utilization of every single machine. What matters is that material, information and work flow through the value stream without unnecessary waiting times.
Lean production distinguishes between three central sources of loss:
Muda: activities that consume resources without creating customer value
Mura: fluctuations and uneven process loads
Muri: overburdening of people, equipment or processes
This distinction matters. Anyone who reduces only visible waste without addressing fluctuations and overburdening often just shifts the problem to another point in the value stream.
How did lean production develop out of industrial practice?
Lean production developed from the goal of building a quality-oriented, flexible and demand-driven production system under limited resources.
Large batch sizes, high inventory levels and long changeover times tie up significant capital and do not fit markets with many product variants. These requirements gave rise to concepts such as just-in-time, jidoka, kanban and standardized work.
The original objective went beyond cost reduction. It combined quality, short lead times and the systematic elimination of process problems. Employees were expected to identify deviations, make them visible and resolve them permanently together with management.
Modern lean approaches take this thinking further. Alongside material flow and machine utilization, they also consider customer needs, employee empowerment, ergonomics, workplace safety and organizational learning. In this way, lean production supports both quality management and safe, reliable work processes.
How do lean management and lean production differ?
Lean management is the overarching leadership and management philosophy, while lean production applies these principles to manufacturing and production-related processes. Lean production is therefore a subset of lean management.
Lean management also covers development, purchasing, logistics, sales, administration and service. Lean production, by contrast, focuses on value streams on the shopfloor, for example machining, assembly, inspection, material supply and maintenance.
Methods such as continuous improvement, kaizen, 5S, gemba walks, value stream mapping, poka yoke and visual management are not standalone lean systems. They serve as tools to implement the lean principles in their respective area of application.
| Level | Focus | Typical methods and metrics |
|---|---|---|
| Lean management | Customer-oriented, waste-conscious company leadership | Hoshin kanri, continuous improvement, gemba walks, lead time, on-time delivery |
| Lean production | Stable material and information flow in manufacturing | 5S, kanban, poka yoke, TPM, OEE, scrap rate, first pass yield |
In practice, an overarching lean management framework combined with concrete lean production goals for the shopfloor works best. Individual methods without a shared direction tend to create isolated improvement projects whose impact stops at department boundaries.
What are the five core principles of lean production?
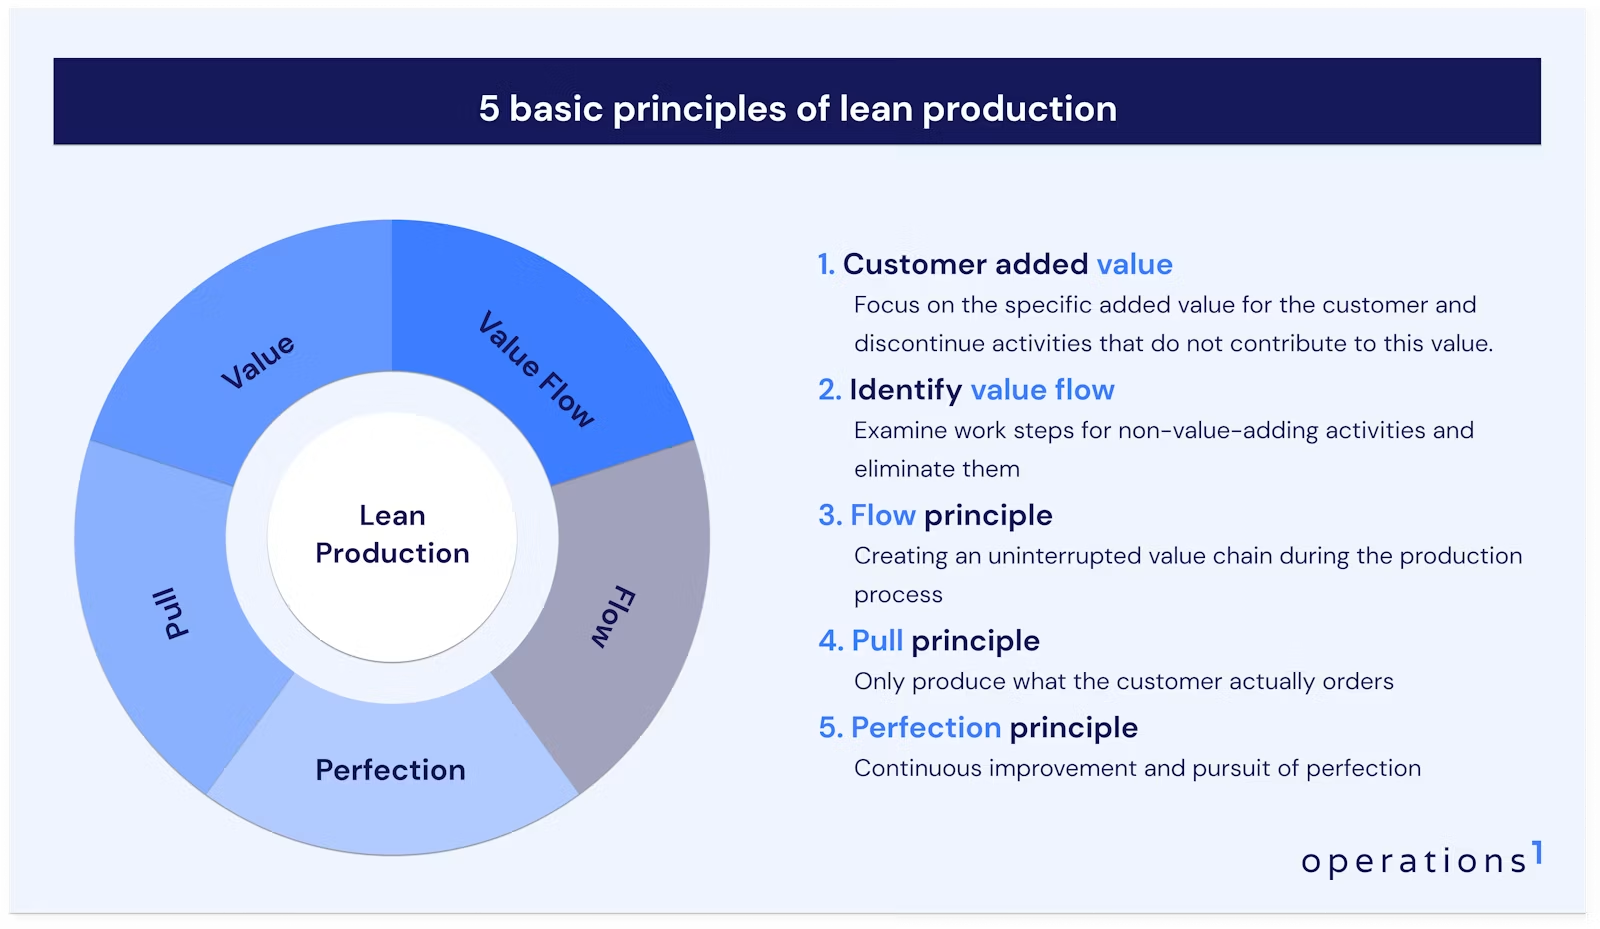
The five lean production principles are value, value stream, flow, pull and perfection. Together they form a connected roadmap: define customer value, examine the value stream, establish flow, produce based on actual demand and continuously improve processes.
| Principle | Guiding question | Operational goal |
|---|---|---|
| Value | What is the customer willing to pay for? | Secure customer-relevant quality, function and delivery performance |
| Value stream | Which steps create value, and which create waste? | Make the entire order flow transparent |
| Flow | Where does the process get interrupted? | Eliminate waiting times, loopbacks and disruptions |
| Pull | What actual demand triggers production? | Limit inventory and overproduction |
| Perfection | How does the process keep getting better? | Turn deviations systematically into improvements |
The sequence itself carries information. Without a clear definition of customer value, it stays unclear which activities truly add value. Without value stream transparency, flow and pull cannot be designed reliably. Perfection, finally, ensures that the improvements achieved are not lost again.
How does the value principle put customer benefit first?
The value principle defines value exclusively from the customer's perspective. An activity is value-adding when it changes the product in the intended way, is done right the first time, and the customer pays for the result.
Depending on the product, customer value can include function, dimensional accuracy, surface quality, traceability, price and delivery date. For an automotive supplier, documented inspection characteristics and compliance with customer-specific requirements are added on top. In medical technology, process safety and complete documentation stand alongside function and quality.
Not every necessary activity creates immediate customer value. Legally required inspections, setup procedures or documentation steps remain necessary regardless. Lean production therefore distinguishes between value-adding activities, currently unavoidable support processes and avoidable waste.
The most common mistake is equating value with internal efficiency. Running a machine faster does not create additional customer value if it produces intermediate inventory, quality problems or longer lead times as a result.
How does value stream mapping make waste visible?
The value stream covers all material and information steps a product goes through from order to delivery. Value stream mapping checks every step to see whether it creates customer value, is necessary, or should be eliminated.
The analysis does not stop at department boundaries. It looks at order release, material supply, setup, machining, assembly, inspection, rework and shipping, among other steps. Only this end-to-end view shows whether local optimizations actually speed up the overall process.
The seven types of waste, often referred to as the 7+1 wastes of lean production, provide a structured way to search for waste:
Overproduction: manufacturing without actual demand or too far ahead of demand
Inventory: excessive amounts of raw material, work in progress or finished goods
Waiting: downtime caused by missing material, approvals, information or tools
Unnecessary transport: additional material movement that adds no value
Unnecessary motion: searching, long walking distances or ergonomically poor movements
Overprocessing: process steps or quality features with no customer benefit
Defects: scrap, rework, sorting activities and complaints
Many companies add an eighth type of waste: unused employee knowledge. This addition matters because workers often spot process deviations earlier than central planning departments do.
The key is distinguishing between symptom and root cause. A waiting time cannot be eliminated permanently if the underlying cause lies in fluctuating material supply, unclear work standards or frequent equipment failures. Fishbone diagrams, 5-why analysis, FMEA and 8D support the subsequent root cause analysis.
How does the flow principle create uninterrupted value creation?
The flow principle aligns processes so that products and information move through manufacturing with as few waiting times, loopbacks and unnecessary buffers as possible. The goal is a stable overall process, not the isolated maximization of individual machine utilization.
Flow disruptions arise, for example, from missing work instructions, long setup times, material shortages, unplanned equipment downtime, quality inspections placed at the end of the process, or unclear approvals. Every interruption extends lead time and increases the effort needed to manage the process.
Typical measures for improving flow include smaller batch sizes, standardized work, leveled production schedules, short distances, quality-assured handovers and preventive maintenance through TPM. Metrics such as lead time, work in progress, first pass yield, OEE and MTTR each capture a different aspect of process performance. No single metric captures flow on its own.
In practice, continuous one-piece flow works best where takt times, product variants and equipment layout support it. Process industries, long processing cycles or technically required batch production call for different flow concepts. Lean does not demand theoretical purity here, but the most economically and technically sound reduction of interruptions.
How does the pull principle replace forecast-driven production?
Under the pull principle, actual demand triggers manufacturing or material supply. Downstream process steps withdraw the quantity they need, while upstream steps only replenish that quantity.
This sets pull apart from a pure push system, where forecasts and central production plans push orders through manufacturing regardless of actual consumption. Pull limits work-in-progress inventory and makes disruptions visible faster, because large buffers no longer mask missing material.
Kanban is a widely used tool for pull control. Supermarkets, FIFO lanes and defined replenishment rules decouple processes where continuous flow is not technically achievable.
Pull does not mean that every product is fully manufactured only after an end customer order arrives. For standard parts with stable consumption, a consumption-driven replenishment approach makes economic sense. For customer-specific variants, order-based assembly is more appropriate. What matters is that actual consumption, not uncontrolled utilization logic, drives replenishment.
Why is perfection a continuous leadership task?
The perfection principle treats lean production not as an end state to reach but as an ongoing improvement of quality, delivery performance, cost, safety and working conditions. Kaizen and continuous improvement translate this principle into daily routines.
Process standards form the starting point. Without a defined target process, a deviation stays invisible and an improvement cannot be assessed objectively. After a successful change, the responsible team updates the standard, trains the affected employees and monitors the effect using suitable metrics.
Continuous improvement relies on short feedback loops. Employees report a deviation, the shift supervisor prioritizes the issue, the team analyzes the root cause and implements a verifiable countermeasure. Larger quality problems require structured methods such as 8D or DMAIC. Smaller obstacles can be resolved directly through shopfloor management.
A culture that does not treat deviations as personal failure is essential here. Anyone who surfaces a problem provides the basis for improvement. A leadership culture that punishes bad news produces good-looking metrics but not a reliable process.
Why do paper-based work instructions hold back the lean principles?
Paper-based work instructions are slow to update, hard to provide variant-specifically and only partly analyzable. Outdated documents, time spent searching and manual documentation interrupt flow and increase the risk of errors and rework.
Many companies already run orders through ERP or MES systems but still hand out work, assembly and inspection instructions on paper on the shopfloor. This creates a media break between digital planning and operational execution.
| Criterion | Paper-based instruction | Digital worker guidance |
|---|---|---|
| Currency | Replacing and recalling outdated versions requires manual checks | One approved version is available centrally |
| Variant control | Workers must match the document to the variant themselves | The system shows order- and variant-specific content |
| Clarity | Text and static images dominate | Images, videos, graphics and multiple languages support the process |
| Feedback | Responsible staff must transfer or evaluate entries manually | Process and inspection data flow back in a structured way |
| Record-keeping | Forms can be lost or filled out incompletely | Required fields and plausibility rules secure the documentation |
| Change process | Responsible staff must replace printouts at every location | Changes are published in a controlled way |
Paper remains sufficient for simple, rarely changed workflows that carry no documentation requirement. With high variant diversity, frequent changes, complex inspection requirements or traceability needs, digital worker guidance is the better option. It reduces the media break and connects planning, execution and feedback in one controlled information flow.
What errors and follow-up costs result from outdated or unclear instructions?
Outdated or unclear instructions lead to incorrect work steps, skipped inspections and faulty parameters. The consequences range from lost productivity to scrap, rework, customer complaints and disrupted on-time delivery.
Simply searching for the right information already creates waste. Workers interrupt their work, ask the shift supervisor, or compare several document versions. The process loses its rhythm while downstream stations wait for parts.
Errors that only surface at the end of the line or with the customer are especially critical. Direct and indirect follow-up costs include:
material loss through scrap
additional labor time for rework and sorting
machine time used outside the production plan
blocked inventory and delayed deliveries
analysis effort through quality management and 8D processes
complaints, warranty claims and loss of customer trust
missing or unreliable evidence during audits
A dysfunctional value stream does not result from faulty documents alone. Unclear responsibilities, unstable master data and inadequate approval processes also play a role. Digitalizing a bad instruction therefore only makes the process bad faster. Before any technical implementation, production, quality and industrial engineering need to clarify the target process.
How do worker assistance systems put the lean principles into digital practice?
Worker assistance systems guide employees step by step through manufacturing, assembly, inspection and maintenance processes. They deliver the right information for a specific order, in an understandable form, at the relevant workstation, and capture feedback directly during execution.
Such a system connects digital work instructions with process data. It provides work instructions and checklists based on the order, guides employees through defined steps and captures input directly in the process. Mandatory steps, limit values and tolerance checks support standardized work and poka yoke.
Worker assistance replaces neither process design nor leadership. The system only delivers value once responsible teams maintain work standards, release changes in a controlled way and actually use the captured data for continuous improvement.
How does digital worker guidance secure customer value under the value principle?
Digital worker guidance secures value by providing only the relevant work, quality and safety information for each order. Variant-specific content reduces misinterpretation and directs execution toward customer-relevant features.
The system can take order and product data from ERP or MES. Based on this, it shows the matching work steps, bill of materials items, torque values, inspection characteristics and drawings. Workers no longer need to search extensive documents for information.
Visual content makes clear communication easier. Images mark installation positions, videos show complex manual steps, and graphics clarify inspection points. Multilingual displays support teams with different language skills. For safety-critical or quality-relevant steps, formal training remains necessary regardless.
The key is focusing on what matters. Overloaded instructions slow down work and obscure critical features. Good digital work instructions present standard information concisely and highlight deviations, warnings and customer-specific requirements clearly.
How does a worker assistance system make the value stream transparent?
A worker assistance system captures process data at the point where the work happens. Timestamps, inspection results, deviation reasons and feedback make waiting times, error sources and unnecessary process steps visible across the value stream.
The captured data complements traditional value stream mapping. Instead of relying only on observations and spot checks, responsible teams can analyze recurring patterns across shifts, variants and workstations.
Relevant analyses cover, for example:
processing and waiting times per process step
frequency of queries and reports
abort and repeat rates
error types and affected product variants
inspection results and first pass yield
reasons for missing material or information
improvement suggestions from employees
Transparency must not be confused with continuous performance monitoring of individual people. Lean keeps the focus on process causes. Companies therefore need clear data purposes, role-based access, appropriate retention periods and, where personal data is involved, the involvement of employee representatives.
How does digital worker guidance support stable flow?
Digital worker guidance supports the flow principle especially directly: employees receive the next valid work step without searching, and report disruptions immediately. This reduces information waiting times, queries and avoidable process interruptions.
The system guides workers through the approved sequence and checks input directly. It detects and documents a limit value violation immediately, for instance, so that responsible staff can trigger the defined response. If material is missing or equipment fails, workers can create a task for the responsible shift supervisor, logistics or maintenance team.
Maintenance also benefits from contextual information. Fault reports linked to the equipment, the observed fault pattern and points already checked shorten diagnosis time. Standardized maintenance instructions support TPM and can help lower MTTR for recurring faults.
The greatest benefit occurs at interfaces. When order data arrives automatically, workers document results in the same workflow, and the MES receives the status back, manual data transfer disappears. This is exactly where paper lists and disconnected systems tend to cause the longest delays.
How does a worker assistance system support the pull principle?
A worker assistance system connects operational execution to the actual order or material request. It provides work content for a specific demand and supports fast switching between product variants.
In order-based manufacturing, the ERP or MES can transmit the next released order. Worker guidance then provides the correct variant and inspection sequence. This makes small batch sizes easier and shortens the organizational preparation needed for frequent product changes.
In kanban processes, workers can scan container, material or order identifiers by barcode or QR code and link the digital information to the physical pull signal. However, the system does not replace sound kanban rules or correctly sized supermarkets and replenishment lead times.
Pull needs stable processes. Digital order provisioning alone does not fix fluctuating delivery times, unreliable equipment or inaccurate inventory. Companies should therefore assess bottlenecks and process capability first and then align digital control accordingly.
How does a worker assistance system become a driver for continuous improvement?
Worker assistance systems support perfection when they capture deviations and improvement suggestions in a structured way and feed them into a binding continuous improvement process. The captured data provides a reliable basis for prioritization, root cause analysis and effectiveness checks.
Workers should be able to give feedback directly at the relevant process step. A photo, an error category and a short comment provide more context than a later report without any order reference. The shift supervisor or process owner assesses the input and decides on an immediate action, a root cause analysis, or a change to the standard.
A closed improvement loop includes the following steps:
Employees record a deviation at the process step.
The system assigns order, variant, workstation and time.
The responsible process owner prioritizes the report.
The team analyzes the root cause, for example using 5-why or a fishbone diagram.
Responsible staff change the process, equipment or work instruction.
A controlled approval process publishes the new standard.
Metrics and feedback show whether the measure is working.
The recommendation is not to treat feedback as an unstructured idea pool. Clear responsibilities, defined turnaround times and visible feedback to the people who raised the issue keep participation high and turn data capture into a functioning continuous improvement process.
How do ERP, SAP, MES and other systems provide the data foundation for lean processes?
ERP, MES, inventory management and CRM systems each provide different data for digital lean processes. A worker assistance system connects this planning and master data with operational execution and can feed status, quality and process data back into these systems.
The systems serve different purposes:
ERP systems such as SAP: orders, material master data, bills of materials, routings and inventory
MES: detailed scheduling, machine status, order progress, feedback and production metrics
Inventory management or WMS: storage locations, material movements and replenishment
CRM: customer requirements, order context and sales information
QMS or CAQ: inspection plans, quality characteristics, deviations and complaints
Worker assistance system: context-aware guidance, data capture and interaction on the shopfloor
System boundaries should be clearly defined. Every type of data needs one leading system. If responsible teams maintain item master data simultaneously in ERP, MES and the worker assistance system, conflicting versions and extra coordination effort result.
In practice, event-driven integration works well. A released order transmits the necessary data to worker guidance. Once complete, the system sends back results, quantities, times and quality status. Standardized interfaces and stable identifiers for order, material, workstation and document version reduce integration errors.
Fail-safe operation matters as well. Production-critical instructions must remain available during network interruptions. At the same time, the system must prevent outdated local content from continuing to be used uncontrolled after a change.
How can 5S audits and gemba walks be implemented digitally?
Digital 5S audits and gemba walks capture observations in a structured way at the point where they occur and link them to responsibilities, deadlines and evidence. This turns individual findings into traceable improvement actions.
In a digital 5S audit, a 5S audit checklist software guides users through the five steps: sort, set in order, shine, standardize and sustain. Photos document the condition, scoring criteria ensure comparability, and each action is assigned a responsible person and a deadline.
A gemba walk serves a different purpose. Managers go to the actual place where value is created, observe the process and talk with employees. Digital support should structure this dialogue, not replace it with a checklist to tick off.
Useful digital functions include:
workstation-specific audit templates
photos and markups attached directly to a finding
categorization by safety, quality, delivery or cost topic
a responsible person and deadline for each action
escalation of overdue tasks
effectiveness checks after completion
trend views across areas and audit periods
The most common mistake is a scoring system with no consequences. Many completed audits do not improve a process if the same deviations keep recurring. A combination of standardized capture, binding action tracking and regular root cause analysis for repeat errors works best.
5S audits and gemba walks often produce good findings that then get lost in daily operations because a clear responsibility or deadline is missing. Operations1's task feature addresses exactly this gap. Employees can create a task directly from an operation within a report and assign it to a person or user group. They can set a due date and track status from open through in progress to done. Task templates define, for report types such as quality issues or maintenance needs, which fields are available and which are mandatory. This keeps follow-up actions fully documented. Anyone looking to systematically track recurring deviations from audits should pilot the task feature on a single 5S or gemba process first and check the effectiveness of the resulting actions there.
What other benefits do worker assistance systems offer for satisfaction, transparency and resilience?
Well-designed worker assistance systems ease onboarding, create process clarity and improve responsiveness to change. These benefits only materialize with clear content, stable technology and genuine employee involvement.
New employees receive standardized, visual guidance through the process. This shortens the time until they can work safely and reliably, but it does not replace a skills matrix or hands-on training. For complex or safety-critical tasks, an experienced expert must still confirm competence.
Experienced workers benefit too when variants, changes and rare special cases are clearly presented. Smoother workflows reduce unnecessary queries and frustration. In this way, digital worker guidance contributes to managing the skilled labor shortage and knowledge transfer, without fully replacing the need for expertise.
Process data increases transparency around recurring disruptions, quality deviations and bottlenecks. Production management, quality management and industrial engineering gain a shared data basis. This allows continuous improvement actions to be prioritized more precisely than based on individual impressions alone.
Resilience comes from the ability to adapt quickly. When suppliers change, products change or external shocks occur, responsible teams can update the affected workflows centrally and roll out the new standard to all relevant workstations. This requires solid change management, well-maintained master data and clearly named process owners.
What should companies look for when selecting a worker assistance system?
A suitable digital worker assistance system needs to reflect real shopfloor processes clearly, integrate with existing IT systems and manage change in a controlled way. Selection should start with process requirements, not with the longest possible feature list.
A reliable selection process follows a clear sequence:
Define the use case and goal: Determine whether the system will support assembly, inspection, maintenance, training or several processes. Set measurable goals such as less rework, shorter onboarding or more complete documentation.
Check process stability: Clarify the target workflow, variant logic, roles and exceptions. An unstable or unclear process is not suitable as a digital standard.
Evaluate shopfloor fitness: Check usability with gloves, readability, device classes, multilingual support, scanning functions and behavior during network interruptions.
Clarify content creation and governance: Departments should be able to create and maintain instructions without programming. Roles, approvals, versioning and change records must be clearly regulated.
Test variant and process logic: The system should control content based on order, product and workstation, and check qualifications. A simple PDF display is not enough for complex processes.
Secure integration: Test interfaces to ERP, SAP, MES, QMS or WMS with real data. Data ownership, error handling and feedback loops matter more than the technical connection alone.
Assess quality and traceability: Required fields, plausibility checks, measurement capture, digital signatures and audit trails must match the relevant industry requirements.
Define data protection and IT security: Role-based access, authentication, encryption, logging, data minimization and deletion concepts belong in the assessment. Where personal data is analyzed, employee representatives should be involved early.
Plan a pilot and scale-up: Test a representative process including variants, disruptions and shift changes. Then evaluate target metrics, user feedback, maintenance effort and integration stability before rolling out to further areas.
The concrete recommendation is: choose not the system with the most features, but the one that demonstrably supports a prioritized value stream and that departments can master over the long term. A limited pilot with real orders provides a much more reliable basis for decision-making than a demo or an isolated feature test alone.